Invert Syrup with Invertase: Bulk Enzyme Supply for Syrup Makers
Invertase for invert syrup makers and resellers: process conditions, trial dosing, shelf life, QC and what to send for a wholesale quote.
Wholesale invertase for syrup producers, confectionery and bakery manufacturers, and ingredient resellers who make invert syrup in-house or sell the enzyme on. This guide covers how plants trial and dose the enzyme, what to check, and what to send for a quote: the product, the quantity and the destination country.
Why invertase matters in invert syrup production
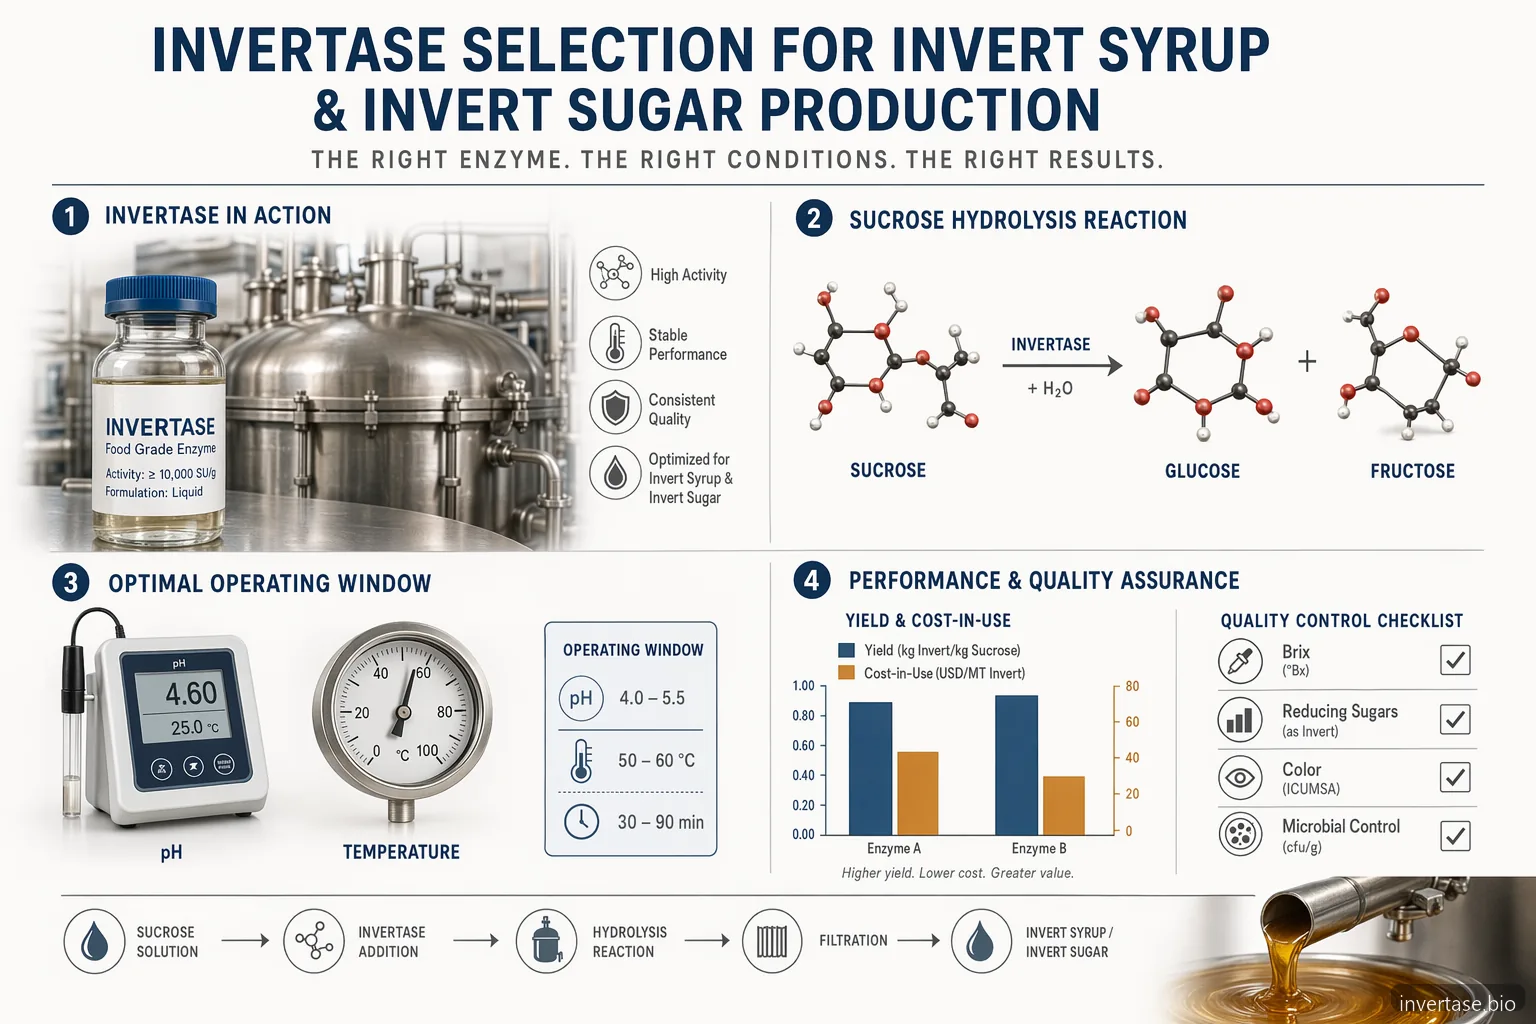
Invertase, also known as sucrase, is the enzyme used to split sucrose into glucose and fructose. In industrial invert syrup production, this enzymatic route can provide controlled inversion under mild processing conditions compared with acid inversion. Buyers typically evaluate invertase for invert sugar when they need predictable sweetness profile, crystallization control, humectancy, and process repeatability for confectionery, bakery, beverage, honey processing, and ingredient applications. For B2B procurement teams, the main question is not simply what is invert sugar, but how consistently a supplier can help produce it at target specifications. A practical invertase enzyme supplier for invert sugar should be able to discuss enzyme activity, application fit, process limits, documentation, logistics, and pilot-scale confirmation before commercial purchase. The best starting point is a clear production target: sucrose conversion level, final Brix, pH, color, flavor neutrality, and shelf-life requirements.
Primary reaction: sucrose plus water to glucose and fructose • Common output: invert syrup or dry invert sugar ingredient streams • Key buyer goal: consistent inversion at acceptable cost-in-use
How Syrup Plants Buy Invertase: Trial First, Then Production Volumes
Food-grade invertase for syrup work is typically produced by submerged liquid fermentation and then refined by ultrafiltration, so ask any supplier which production and refining route a grade uses before you compare activity figures. Grades made this way are listed for general use across the food and beverage sector rather than for a single end use. Food-grade sucrase is sold by the kilogram on trade listings, some with a minimum order as small as 1 kg, so a plant can buy a trial quantity for a pilot batch before it commits to production volumes. One such grade states a 12-month shelf life, so production orders should match what the plant will actually use within a year of delivery. Set the dose in that pilot batch, within the 0.02-0.20% w/w screening range in the FAQ below.
Typical process conditions for enzymatic inversion
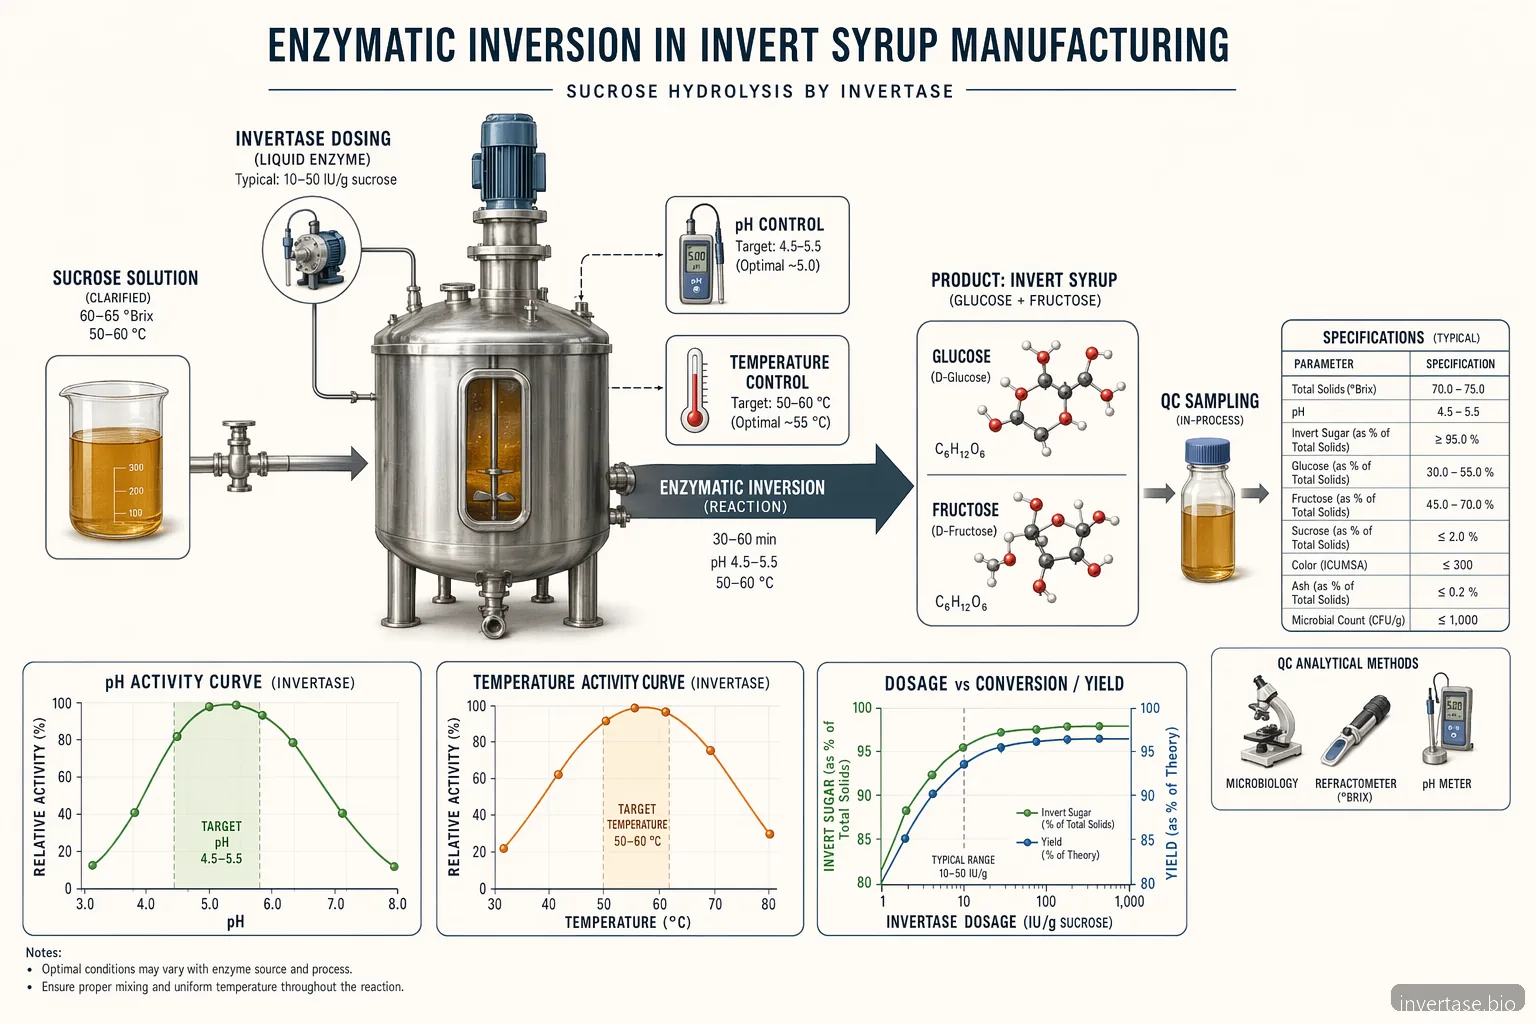
When asking how to invert syrup with invertase enzyme, treat published conditions as a starting range, not a final recipe. Many industrial invertase preparations perform well in mildly acidic syrup systems, commonly around pH 4.0-5.5. Trial temperatures often fall between 45-60°C, depending on the enzyme source, syrup solids, reaction time, and required conversion. Higher solids can slow mass transfer and change viscosity, so laboratory results should be confirmed at pilot scale using plant-equivalent mixing, heating, and holding equipment. Reaction time may range from less than one hour to several hours, depending on dosage and target inversion. After the desired invert sugar profile is reached, processors commonly use heat treatment or downstream processing controls to stop or reduce residual activity, subject to product and regulatory requirements. Always confirm safe handling and processing guidance from the supplier TDS and SDS.
Indicative pH: 4.0-5.5 • Indicative temperature: 45-60°C • Confirm endpoint by reducing sugar or HPLC testing
Dosage strategy and cost-in-use
Invertase dosage should be selected by enzyme activity, substrate concentration, residence time, and the commercial endpoint, not by a generic percentage alone. In screening trials, manufacturers may test a dosage band such as 0.02-0.20% w/w enzyme preparation on syrup, then refine based on actual activity units, Brix, pH, and conversion target. A lower dosage may work with longer holding time, while a higher dosage may support faster throughput if heat stability and product quality remain acceptable. Cost-in-use should include enzyme price, activity per gram or milliliter, required dosage, processing time, energy, yield, rework reduction, and losses from off-spec inversion. For buyer comparisons, request enough data to normalize competing offers on delivered activity and performance in your syrup matrix. A low unit price is not always the lowest cost if it requires higher dosing or causes process delays.
Run dose-response trials before setting purchase volume • Compare suppliers by delivered activity and conversion performance • Include holding time and energy in cost-in-use calculations
QC checks for invert syrup and invert sugar
Quality control should verify both enzyme performance and finished syrup specifications. Common checks include incoming enzyme activity, appearance, odor, pH, and COA review. During production, operators may monitor Brix, pH, temperature, reaction time, and sample-based conversion. Finished invert syrup QC can include reducing sugars, residual sucrose, glucose-to-fructose profile, color, turbidity, ash, sensory evaluation, and microbial limits appropriate to the product category. HPLC is useful when a detailed sugar profile is required, while titration-based reducing sugar methods may be suitable for routine process control if validated. For confectionery applications, crystallization behavior and water activity may be as important as chemical conversion. For honey processing, buyers should validate that enzyme use fits product standards and labeling requirements in the target market. Maintain retention samples and batch records to support traceability and troubleshooting.
Incoming: activity, COA match, packaging integrity • In-process: Brix, pH, temperature, conversion • Finished: residual sucrose, reducing sugars, microbial quality
How to qualify an invertase supplier
An invertase supplier for invert sugar should provide more than a price quote. Ask for a current technical data sheet, certificate of analysis, safety data sheet, recommended storage conditions, shelf-life, allergen or carrier information where relevant, and activity assay method. Confirm whether the activity definition is comparable across suppliers; enzyme units are not always interchangeable. Supplier qualification should also cover manufacturing consistency, change notification practices, lead time, packaging sizes, minimum order quantity, technical support, and the ability to support scale-up. For regulated food applications, procurement and quality teams should review documentation against internal requirements and local rules rather than relying on unsupported claims. If the supplier offers application guidance, use it to design a pilot protocol, but verify results in your own formulation. The strongest supplier relationship is built on transparent data, repeatable batches, and responsive technical communication.
Request COA, TDS, SDS, and activity method • Review change control and traceability expectations • Validate performance before commercial approval
Application fit: confectionery, syrups, and honey processing
Invert syrup is widely used where sweetness, moisture retention, and crystallization control are important. In confectionery, invertase confectionery supplier for invert sugar searches often come from manufacturers of fondants, creams, fillings, cordials, and soft-centered products. In these systems, enzyme dosage and residual activity can affect texture development over time, so shelf-life studies are essential. For bulk invert sugar syrup, the focus is usually conversion efficiency, color control, viscosity management, and microbial stability. In honey processing or honey-style blends, invertase may be evaluated for sucrose reduction or sugar profile adjustment, but buyers must confirm compliance with product identity, labeling, and regional standards. Across applications, the same principle applies: match the invertase enzyme for invert sugar to the exact matrix, solids level, pH, heat profile, and finished-product specification. A qualified supplier should help translate lab data into plant-ready trials.
Confectionery: texture, crystallization, and shelf-life validation • Syrup plants: conversion, throughput, and consistency • Honey processing: confirm standards and labeling requirements
Request a Quote: What to Send
To request a quote, send the grade (powder or liquid), the quantity per order or per year, the destination country, and your syrup strength and target inversion. A trial quantity for a pilot batch can be quoted before a production order. Email hello@mail.invertase.bio or use the form. Prices and lead times are quoted per order.
Buyer Questions
Invert sugar is a mixture of glucose and fructose made by hydrolyzing sucrose. Invertase enzyme catalyzes this reaction under controlled, mildly acidic processing conditions. Manufacturers use invertase for invert sugar when they need a specific sweetness profile, improved moisture retention, reduced sucrose crystallization, or repeatable syrup performance. Final benefits depend on formulation, conversion level, solids, pH, and storage conditions.
Choose a supplier that can provide a clear activity specification, COA, TDS, SDS, shelf-life, storage guidance, and technical support for pilot trials. Ask how activity is measured, whether batch-to-batch data are available, and what change notification practices apply. The supplier should help you evaluate dosage, conversion, process fit, and cost-in-use without making unsupported claims.
A common starting window for invert syrup trials is pH 4.0-5.5 and 45-60°C. The best setting depends on the enzyme grade, syrup Brix, target inversion, holding time, and product quality limits. High solids and viscosity can slow reaction performance, so lab results should be confirmed in pilot equipment with representative mixing, heating, and sampling.
There is no universal dosage because invertase preparations differ in activity and formulation. Many buyers begin with screening trials around 0.02-0.20% w/w enzyme preparation on syrup, then adjust by measured activity units, conversion target, temperature, pH, and residence time. The best commercial dose is the one that reaches specification reliably at the lowest validated cost-in-use.
Important QC checks include incoming enzyme activity, COA verification, pH, Brix, reaction temperature, conversion rate, reducing sugars, residual sucrose, color, odor, and microbial quality. HPLC can provide a detailed glucose, fructose, and sucrose profile when needed. For confectionery, also validate crystallization behavior, texture change, water activity, and shelf-life under intended storage conditions.
Request a quote: wholesale and bulk invertase
For manufacturers, distributors and resellers. Send the product and grade (powder or liquid), the quantity per order or per year, the destination country and your application. We reply within 24 hours with a grade recommendation and a quote per order, and send samples with COA/TDS for qualified inquiries.
Frequently Asked Questions
How do syrup plants usually order invertase?
Most start with a trial quantity for a pilot batch at their own syrup strength and hold time, set the dose from that run, and then order production volumes sized to what they will use within the stated shelf life. Tell us your yearly volume and we will quote per order.
What is invert sugar and why use invertase?
Invert sugar is a mixture of glucose and fructose made by hydrolyzing sucrose. Invertase enzyme catalyzes this reaction under controlled, mildly acidic processing conditions. Manufacturers use invertase for invert sugar when they need a specific sweetness profile, improved moisture retention, reduced sucrose crystallization, or repeatable syrup performance. Final benefits depend on formulation, conversion level, solids, pH, and storage conditions.
How do I choose an invertase enzyme supplier for invert sugar?
Choose a supplier that can provide a clear activity specification, COA, TDS, SDS, shelf-life, storage guidance, and technical support for pilot trials. Ask how activity is measured, whether batch-to-batch data are available, and what change notification practices apply. The supplier should help you evaluate dosage, conversion, process fit, and cost-in-use without making unsupported claims.
What pH and temperature should I use for invert syrup?
A common starting window for invert syrup trials is pH 4.0-5.5 and 45-60°C. The best setting depends on the enzyme grade, syrup Brix, target inversion, holding time, and product quality limits. High solids and viscosity can slow reaction performance, so lab results should be confirmed in pilot equipment with representative mixing, heating, and sampling.
How much invertase is needed to invert syrup?
There is no universal dosage because invertase preparations differ in activity and formulation. Many buyers begin with screening trials around 0.02-0.20% w/w enzyme preparation on syrup, then adjust by measured activity units, conversion target, temperature, pH, and residence time. The best commercial dose is the one that reaches specification reliably at the lowest validated cost-in-use.
What QC tests are important for industrial invert syrup?
Important QC checks include incoming enzyme activity, COA verification, pH, Brix, reaction temperature, conversion rate, reducing sugars, residual sucrose, color, odor, and microbial quality. HPLC can provide a detailed glucose, fructose, and sucrose profile when needed. For confectionery, also validate crystallization behavior, texture change, water activity, and shelf-life under intended storage conditions.
Related: Invertase for Invert Sugar Syrup Production — Enzymatic Sucrose Conversion for Food Manufacturing
Turn This Guide Into a Supplier Brief Request invertase specifications, samples, and pilot support for your invert syrup process. See our application page for Invertase for Invert Sugar Syrup Production — Enzymatic Sucrose Conversion for Food Manufacturing at /applications/invertase-invert-sugar-syrup-production/ for specs, MOQ, and a free 50 g sample.
Request a quote: wholesale and bulk invertasehello@mail.invertase.bio